Every container, checked.
Without opening a single one.
Thermography and artificial intelligence inspection that verifies the seal of 100 % of your production at your line speed. Badly sealed containers are rejected before they leave the factory.
Thermal inspection: every container, verified.
An induction seal leaves a thermal signature. Thermographic cameras capture it as each container passes, and artificial intelligence compares it in real time with the pattern of a correct seal: if a container hasn't sealed properly, it is detected and rejected in line, without slowing production.
Without stopping the container. Without opening the cap. No sampling: 100 % of production is inspected.
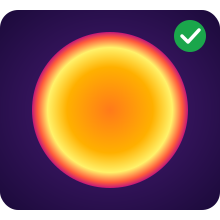
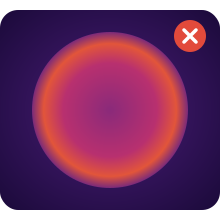
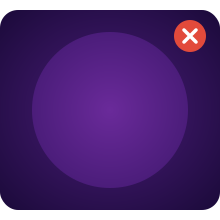
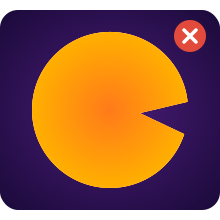
Sealing faults cause a change in the temperature pattern, and that change can be detected.
What it detects
Sealing faults have three origins. Thermal inspection detects the faults, container by container. And it learns: a new error is taught to the system.
- High temperature: excess power, melted or burnt areas
- Low temperature: insufficient power to seal
- Wrong or unsuitable coil
- Poorly adjusted power
- Incorrectly adjusted distance to the container
- Excessive or variable conveyor speed
- Misaligned sealer
- Crooked or overtightened cap
- Insufficient or irregular closing torque
- Uneven pressure: cap mould without a flat zone, thread without 360° contact, deformed container or cap
- Irregular sealing area
- Sealing area contaminated by the product
- Missing liner
- Broken, torn or folded liner
- Double liner
- Inverted liner
- Off-centre liner
- Liner not in contact with the container mouth
- Incompatible container and liner materials
And the most useful part: every fault points to its cause. Those that originate with the operator — wrong coil, power or distance incorrectly adjusted, conveyor speed changed — are corrected with parameter-based training. Those that come from another machine on the line — crooked or overtightened cap from the capping machine, irregular closing torque, sealing area stained by the filler — are resolved upstream, not at the sealer. Those from the sealer itself — excess or shortage of temperature, misalignment — show up in the thermal signature before they affect production. And those from the materials — missing, broken, double or inverted liner, cap mould without a flat zone, deformed container, incompatible materials — already arrive from your supplier: detecting them in time avoids returns and lets you make a claim backed by data. Knowing where the error comes from is half the battle of solving it.
Integrated into your line.
It is placed over your conveyor, after the sealer, and works in coordination with it: interlock, error signals, automatic rejection of the badly sealed container, image recording and line stop on repeated errors. Sealing traceability, container by container.